

Solution Manual For Matching Supply with Demand: An Introduction to Operations Management, 4th Edition
- Operations Management
- 76 pages
- Shared February 2025
- 36 downloads
Solution Manual For Matching Supply with Demand: An Introduction to Operations Management, 4th Edition gives you the answers you need, explained in a simple and clear way.
Preview 23 of 76 pages
See the first 23 pages exactly as they appear in the document.
Page 1 Read page 1 as text
2 - 1 Matching Supply with Demand: An Introduction to Operations Management 4e Solutions to Chapter Problems Chapter 2 The Process View of the Organization Q2.1 Dell The following steps refer directly to Exhibit 2.1. #1: For 2001, we find in Dell’s 10 - k: Inventory=$400 (in million) #2: For 2001, we find in Dell’s 10 - k: COGS=$ 26,442 (in million) #3: Inventory turns= $ 400 / $ 442 , 26 year = 66.105 turns per year #4: Per unit Inventory cost = year per 66.105 year per 40% = 0.605% per year Q2.2. Airline We use Little’s law to compute the flow time, since we know both the flow rate as well as the inventory level: Flow Time = Inventory / Flow Rate = 35 passengers / 255 passengers per hour = 0.137 hours = 8.24 minutes Q2.3 Inventory Cost (a) Sales = $60,000,000 per year / $2000 per unit = 30,000 units sold per year Inventory = $20,000,000 / $1000 per unit = 20,000 units in inventory Flow Time = Inventory / Flow Rate = 20,000 / 30,000 per year = 2/3 year = 8 months Turns = 1 / Flow Time = 1 / (2/3 year) = 1.5 turns per year Note: we can also get this number directly by writing: Inventory turns=COGS/ Inventory (b) Cost of Inventory: 25% per year / 1.5 turns=16.66%. For a $1000 product, this would make an absolute inventory cost of $166.66. Q2.4. Apparel Retailing (a) Revenue of $100M implies COGS of $50M (because of the 100% markup). Turns = COGS/Inventory = $50M/$5M = 10.
Page 2 Page 3 Read page 3 as text
2 - 2 (b) The inventory cost, given 10 turns, is 40%/10 = 4%. F or a 30$ item, the inventory cost is 0.4 x $30 = $1.20 per unit . Q2.5. La Villa (a) Flow Rate = Inventory / Flow Time = 1200 skiers / 10 days = 120 skiers per day (b) Last year: on any given day, 10% (1 of 10) of skiers are on their first day of skiing This year: on any given day, 20% (1 of 5) of skiers are on their first day of skiing Average amount spent in local restaurants (per skier) Last year = 0.1 * $50 + 0.9 * $30 = $32 This year = 0.2 * $50 + 0.8 * $30 = $34 % change = ($34 - $32) / $32 = 6.25% increase Q2.6. Highway We look at 1 mile of highway as our process. Since the speed is 60 miles per hour, it takes a car 1 minute to travel through the process (flow time). There are 24 cars on ¼ of a mile, i.e. there are 96 cars on the 1 mile stretch (inventory). Inventory=Flow Rate * Flow Time: 96 cars=Flow Rate * 1 minute Thus, the Flow Rate is 96 cars per minute, corresponding to 96*60=5760 cars per hour. Q2.7. Strohrmann Baking The bread needs to be in the oven for 12 minutes (flow time). We want to produce at a flow rate of 4000 breads per hour, or 4000/60=66.66 breads per minute. Inventory=Flow Rate * Flow Time: Inventory=66.66 breads per minute* 12 minutes Thus, Inventory =800 breads, which is the required size of the oven. Q2.8. Mt Kinley Consulting We have the following information available from the question: Level Inventory (number of consultants at that level) Flow Time (time spent at that level) Associate 200 4 years Manager 60 6 years Partner 20 10 years (a) We can use Little’s law to find the flow rate for associate consultants: Inventory=Flow Rate * Flow Time; 200 consultants=Flow Rate * 4 years; thus, the flow rate is 50 consultants per year, which need to be recruited to keep the firm in its current size (note: while there are also 50 consultants leaving the associate level, this says
Page 4 Read page 4 as text
2 - 3 nothing about how many of them are dismissed vs how many of them are promoted to Manager level). (b) We can perform a similar analysis at the manager level, which indicates that the flow rate there is 10 consultants. In order to have 10 consultants as a flow rate at the manager level, we need to promote 10 associates to manager level (remember, the firm is not recruiting to the higher ranks from the outside). Hence, every year, we dismiss 40 associates and promote 10 associates to the manager level (the odds at that level are 20%) Now, consider the partner level. The flow rate there is 2 consultants per year (obtained via the same calculations as before). Thus, from the 10 manager cases we evaluate every year, 8 are dismissed and 2 are promoted to partner (the odds at that level are thereby also 20%). In order to find the odds of a new hire to become partner, we need to multiply the promotion probabilities: 0.2*0.2=0.04. Thus, a new hire has a 4% chance of making it to partner. Q2.9. Major US Retailers a. Product stays on average for 31.9 days in Costco’s inventory b. Costco has for a $5 product an inventory cost of $0.1311 which compares to a $0.2049 at Wal - Mart Q2.10. McDonald’s a. Inventory turns for McDonald’s were 92.3. They were 30.05 for Wendy’s. b. McDonald’s has per unit inventory costs of 0.32%, which for a 3$ meal about $0.00975. That compares to 0.998% at Wendy’s where the cost per meal is $0.0299. Q2.1 1 . BCH I = 400 associates, T = 2years. R = I / T = 400 associates / 2 yrs = 200 associates/yr. Q2.1 2 . Kroger Turns = R / I = 76858 / 6244 = 12.3
Page 5 Read page 5 as text
Last revised May 2018 3 - 1 Matching Supply with Demand: An Introduction to Operations Management 4e Solutions to Chapter Problems Chapter 3 Understanding the Supply Process: Evaluating Process Capacity Q3.1 Process Analysis with One Flow Unit (a) Capacity of the three resources in units per hour are 60 * 2 / 10 = 12, 60 *1 / 6 = 10; 60 * 3 / 16 = 11.25. The bottleneck is the resource with the lowest capacity, which is resource 2. (b) The process capacity is the capacity of the bottleneck, which is 10 units/hr. (c) If demand = 8 units/hr, then the process is demand constrained and the flow rate is 8 units/hr (d) Utilization = Flow Rate / Capacity. For the three resources they are 8 / 12, 8 / 10, and 8 / 11.25. Q3. 2 Process Analysis with Multiple F low Unit s a) Bottleneck is resource 3 because it has the highest implied utilization of 125%. The demands per hour of the three products are 40/8 = 5, 50/8 = 6.25 and 60/8 = 7.5. The total minutes of work demanded per hour at resource 1 is 5 x 5 + 6.25 * 5 + 7.5 * 5 = 93.75. Two workers at resource 1 produce 2 * 60 = 120 min of work per hour. So resource 1’s utilization is 93.75 / 120 = 0.78. Utilization at the other resources are similarly evaluated. b) The capacity of resource 3 is 60 / 15 = 4 units per hour. Given the ratio of units produced must be 4 to 5 to 6, the process can produce 4 units/ hr of A, 5 units/hr of B and 6 units/hr of C. Q3.3. Cranberry Cranberries arrive at a rate of 150 barrels per hour. They get processed at a rate of 100 barrels per hour. Thus, inventory accumulates at a rate of 150 - 100=50 barrels per hour. This happens while trucks arrive, i.e. from 6am to 2pm. The highest inventory level thereby is 8h*50 barrels per hour=400 barrels. From these 400 barrels, 200 barrels are in the bins, the other 200 barrels are in trucks. (a) 200 barrels (b) From 2pm onwards, no additional cranberries are received. Inventory gets depleted at a rate of 100 barrels per hour. Thus, it will take 2h until the inventory level has dropped to 200 barrels, at which time all waiting cranberries can be stored in the bins (no more truck waiting) (c) It will take another 2 hours until all the bins are empty (d) Since the seasonal workers only start at 10:00am, the first 4 hours of the day we accumulate 4hours * 50barrels per hour=200 barrels. For the remaining time that we receive incoming
Page 6 Read page 6 as text
Last revised May 2018 3 - 2 cranberries, our processing rate is higher (125 barrels per hour). Thus, inventory only accumulates at a rate of 25 (150 - 125 barrels per hour). Given that this happens over 4 hours, we get another 100 barrels in inventory. At 2pm, we thereby have 300 barrels in inventory. After 2pm, we receive no further cranberries, yet we initially process cranberries at a rate of 125 barrels per hour. Thus, it only takes 100 barrels / 125 barrels/hour=0.8 h ours=48 minutes until all bins are empty. From then, we need another 2h until the bins are empty. Q3.4. Western Pennsylvania Milk We start the day with 25,000 gallons of milk in inventory. From 8am onwards, we produce 5,000 gallons, yet we ship 10,000 gallons. Thus inventory is depleted at a rate of 5000 gallons per hour, which leaves us without milk after 5 hours (at 1pm). From then onwards, clients will have to wait. This situation gets worse and worse and by 6pm (last client arrives), we are short 25,000 gallons. (a) 1pm (b) Clients will stop waiting when we have worked off our 25,000 gallon backlog that we are facing at 6pm. Since we are doing this at a rate of 5,000 gallon per hour, clients will stop waiting at 11pm (after 5 more hours). (c) At 6pm, we have a backlog of 25,000 gallons, which is equivalent to 20 trucks (d) The waiting time is the area in the triangle - width: beginning of waiting (1pm) to end of waiting (11pm)=10 hours - height: maximum number of trucks waiting: 20 (see part c above) Hence, we can compute the area in the triangle as: 0.5*10hours*20trucks=100 truck* hours The cost for this waiting is 50$/truck* hour * 100 truck hours=5000$ Q3.5. Bagel Store (a) The bottleneck is “Veggies on Bagel”, as it has the highest implied utilization. Resource Available minutes per hour Grilled veggie bagel Veggie bagel Cream cheese bagel Total Implied utilization Cut 60 3*3 3*11 3*4 54 54/60 Grilled stuff 60 3*10 0 0 3 0 30/60 Veggies on Bagel 60 3*5 11*5 0 70 70/60 Cream cheese 60 0 0 4*4 16 16/60 Wrap 60 3*2 11*2 4*2 36 36/60 (b) If we want to keep the product mix constant (i.e. keep the ration between the various bagel types at 3:11:4), we need to scale down demand by 60/70. This leads to the following flow rates: - Grilled veggie: 3*60/70 bagels / hour
Page 7 Read page 7 as text
Last revised May 2018 3 - 3 - Veggie: 11*60/70 bagels / hour - Cream cheese: 4*60/70 bagels / hour If we try to fulfill as much demand as possible, we encounter a problem with Veggie bagels and Grilled+Veggie bagels. Given that we have an implied utilization of 70/60% at the bottleneck, we can only fulfill 60/70% of demand for these two bagel types. We can meet all of demand for the cream cheese bagels. Q3.6. Valley Forge Income Tax Recall that the demand for the 4 groups is: 1: 15% 2: 5% 3: 50% 4:30% There are three resources, the admin, the junior person, and the senior person. We compute the minutes of capacity they have available every month as well as their work - load, given that there are 50 incoming returns to be processed. This leads to the following computations. Resource Minutes per month 1 2 3 4 Total work - load Implied utilization Admin 9600 0.15*50 *(20+50) 0.05*50 *(40+80) 0.5*50 *(20+30) 0.3*50 *(40+60) 3575 0.372 Senior 9600 0.15*50 *(30+20) 0.05*50 *(90+60) 0.5*50 *(0+5) 0.3*50 *(0+30) 1325 0.138 Junior 9600 0.15*50 *120 0.05*50 *300 0.5*50 *80 0.3*50 *200 6650 0.693 (a) The junior person is the bottleneck, her implied utilization is the highest (b) Implied utilizations (see table) (c) One should consider: revenue, future revenue (lifetime value of customer), to what extent the request draws on bottleneck capacity (d) not at all, since improvements at non - bottleneck steps don’t increase capacity Q3.7 . Car Wash Supply Process a. The implied utilization at wheel cleaning is: 42 minutes of work from package 3 a day, 84 minutes of work from package 4 per day, giving a total of 126 minutes per day. Relative to 720 minutes of available time, that gives an implied utilization of 17.5%.
Page 8 Read page 8 as text
Last revised May 2018 3 - 4 b. The highest implied utilization is at step 1 (automated washing machine) where the implied utilization is 55.55%. c. The new bottleneck will be the interior cleaning employee with an implied utilization of 111% d. Every day, we are 80 minutes of work short at step “interior cleaning”. That corresponds to four customers with package 4. Q3.8. Starbucks a. Time required of the frozen drink maker = 20*2 = 40 minutes. Each worker has 60 minutes available, so the utilization for the frozen drink maker: 40/60 b. Highest implied utilization is for the Espresso Drink Maker with 116.66% c. The workload on the cashier is as follows. 25 Drip coffee customer per hour at 1/3 min per customer = 25/3 min/hr. 5 Ground customers per hour at 1 min per customer = 5 min/hr. 120 customers per hour at 1/3 min to pay per customer = 40 min/hr. 30% of 120 customers per hour buying food, which is 36 customers per hour and they require 1/3 min per customer, for a total of 12 min/hr. In total the workload on the cashier is 25/3 + 5 + 40 + 12 = 65.33 min/hr. The implied utilization is 65.33 / 60 = 108.9%. The implied utilization of the other persons don’t change and they are 66.66% and 116.66%. Q3.9. Paris Airport a. The implied utilization levels of the resources are computed as follows Servers Avail. Min/Hr Requested Imp. Util. Security 4 240 150 62.50% Agents 6 360 440 122.22% Kiosk 3 180 160 88.89% b. The backlog at the bottleneck accumulates at a rate of 80 “requested minutes” per hour. After 4 hours this is 4*80 = 320 “requested minutes” of work from the agents. This takes 6 agents 320/360 = 8/9 = 0.89 hours to complete, or 53.4 minutes after the last arrival c. When Kim arrives, the backlog is half as long as the final backlog in question 2, e.g. there are 160 “requested minutes” of work in front of Kim. This will take the agents 160/360 = 0.45 hours = 26.6 minutes to complete. Kim takes 3 minutes to complete service with the agent and 30 seconds to pass through security (there is no line at security) so the answer is 30 minutes and 10 seconds d. We compute the new utilizations as follows: Servers Avail. Min/Hr Requested Imp. Util. Security 4 240 150 62.50% Agents 6 360 376 104.44% Kiosk 3 180 32 17.78%
Page 9 Read page 9 as text
Last revised May 2018 3 - 5 Extra work accumulates at a rate of 16 minutes per hour for the agents, for a total of 64 minutes after the last arrival. This takes the 6 agents 64/360 = 0.178 hours = 10.7 minutes to complete, so 8:10 PM is the closest answer.
Page 10 Read page 10 as text
Last revised May 2018 4 - 1 Matching Supply with Demand: An Introduction to Operations Management 4e Solutions to Chapter Problems Chapter 4 Estimating and Reducing Labor Costs Q4.1. Empty System Labor Utilization (a) Time to complete 100 units: #1 The process will take 10+6+16minutes=32 minutes to produce the first unit. #2 We know from problem xyz that resource 2 is the bottleneck and the process capacity is 0.1666 units per minute #3 Time to finish 100 units = 32 minutes s/min 0.1666unit units 99 + =626 minutes (b) + (c) + (d) Use Exhibit for Labor computations #1 Capacities are: Resource 1: 2/10 units/ minute=0.2 units/minute Resource 2: 1/6 units/ minute=0.1666 units/minute Resource 3: 3/16 units/ minute=0.1875 units/minute Resource 2 is the bottleneck and the process capacity is 0.1666 units/minute #2 Since there is unlimited demand, the flow rate is determined by the capacity and thereby 0.1666 units/minute; this corresponds to a cycle time of 6 minutes/unit #3 Cost of direct labor = s/h 0.1666unit * 60 10$/h * 6 =6$/unit #4 Compute the idle time of each worker for each unit: Idle time for workers at resource 1=6min/unit*2 – 10 min/unit=2 min/unit Idle time for worker at resource 2=6min/unit*1 - 6min/unit = 0 min/unit Idle time for workers at resource 3=6min/unit*3 - 16min/unit=2 min/unit #5 Labor content=10+6+16 min/unit=32min/unit
Page 11 Read page 11 as text
Last revised May 2018 4 - 2 #6 Average labor utilization= 4 32 32 + =0.8888 Q4.2. Assign tasks to workers (a) Worker Task(s) Processing Time (sec) Capacity (units per hour) 1 1 30 120 2 2 25 144 3 3,4 75 48 4 5,6 45 80 The capacity of the current line is restricted by the capacity of the step with the longest processing time. Therefore, capacity = 1 / 75 sec = 48 units per hour. (b) Worker Task(s) Processing Time (sec) Capacity (units per hour) 1 1,2 55 65.45 2 3 35 102.86 3 4 40 90 4 5,6 45 80 Therefore, capacity of the revised line = 1 / 55 sec = 65.45 units per hour. (a) No matter how you organize the tasks, maximum capacity of the line is 65.45 units per hour, i.e. at a cycle time of 55 seconds. Q4.3. Power Toys (a) Since every resource has exactly one worker assigned to it, the bottleneck is the assembly station with the highest processing time (#3) (b) Capacity = 1 / 90 sec = 40 units per hour (c) Direct labor cost = Labor cost per hour / flow rate = 9*15 $/h / 40 trucks per hour = 3.38 $/truck (d) Direct labor cost in work cell= (75+85+90+65+70+55+80+65+80) sec/truck * $15/hr = 2.77$/truck (e) Utilization = flow rate / capacity 85 sec / 90 sec = 94.4% (f) Worker Station(s) Processing Time (sec) Capacity (units per hour) 1 1 75 48 2 2 85 42.35
Page 12 Read page 12 as text
Last revised May 2018 4 - 3 3 3 90 40 4 4,5 135 26.67 5 6,7 135 26.67 6 8,9 145 24.83 (g) Capacity = 1 / 145 units/second = 24.83 toy - trucks per hour Q4.4. 12 tasks to 4 workers (a) Worker Task(s) Processing Time (sec) Capacity (units per hour) 1 1,2,3 70 51.43 2 4,5,6 55 65.45 3 7,8,9 85 42.35 4 10,11,12 60 60 (a) Capacity = 1 / 85 sec = 42.35 units per hour (b) Direct labor content = (70+55+85+60) sec = 270 sec/unit or 4.5 min/unit (c) Labor utilization = labor content / (labor content + total idle time) = 270 sec / (270 + 15 + 30+ 0 +25 sec) = 79.41% (d) Note that we are facing a machine paced line, thus the first unit will take 4*85 seconds top go through the empty system. Flow Time = 4 * 85 sec + 99 / (1 / 85 sec) = 8755 sec or 145.92 min or 2.43 hrs (e) There are multiple ways to achieve this capacity. This table shows only one example. Worker Task(s) Processing Time (sec) Capacity (units per hour) 1 1,2 55 65.45 2 3,4,5 50 51.43 3 6,7 70 51.43 4 8,9 35 102.86 5 10,11,12 60 60 Capacity = 1 / 70 units/sec = 51.43 units per hour (f) There are multiple ways to achieve this capacity. This table shows only one example. Worker Task(s) Processing Time (sec) Capacity (units per hour) 1 1,2 55 65.45 2 3,4,6 55 65.45 3 5,8,10 55 65.45 4 7 50 72 5 9,11,12 55 65.45 Capacity = 1 / 55 units/sec = 65.45 units per hour
Page 13 Read page 13 as text
Last revised May 2018 4 - 4 (g) We have to achieve a cycle time of 3600/72=50 seconds/unit. The following task allocation includes a lot of idle time, but is the only way to achieve the cycle time, given the constraints we face. Worker Task(s) Processing Time (sec) 1 1 30 2 2,3 40 3 4,5 35 4 6 20 5 7 50 6 8,9 40 7 10,11 40 8 12 20 Therefore, a minimum of 8 workers are required to achieve a capacity of 72 units per hour. Q4.5. Geneva Watch (a) Station E is the bottleneck with a process capacity of 1 unit every 75 seconds. (b) Capacity = 1 / 75 sec = 48 watches per hour (c) Direct labor content = 68 + 60 + 70 + 58 + 75 + 64 = 395 sec (d) Utilization = 60 sec / 75 sec = 80% (e) Idle time = (75 - 70) sec / 75 sec * 60 min per hour = 4 min per hour ; as an alternative computation, we can observe that the worker has 5 seconds idle time per cycle (i.e. per unit) and that there are 48 cycles (units) per hour. Thus, the idle time over the course of an hour is 240 seconds=4 minutes. (f) Time to produce 193 watches = time for the first watch + time for the remaining 192 watches = 6*75 seconds + 192*75 seconds=14,850 seconds=4h7min30sec. Production begins at 8:00, so 193 watches will be completed by 12:07:30 Q4.6. Yoggo Soft Drink a. Bottling machine capacity: 1 bottles/second Lid machine capacity: 0.333 bottles/sec Two labeling machines capacity: 10/25=0.4 bottles/sec Packaging machine capacity: 0.25 bottles/sec So the process capacity is going to be 0.25bottles/sec=0.25*3600=900 bottles/hour b. The packaging machine
Page 14 Read page 14 as text
Last revised May 2018 4 - 5 c. It has no effect on the capacity since it is not the bottleneck d. Process capacity = 90 boxes/ hour, implied utilization= demand / capacity = 0.666=66% Q4.7. Atlas Inc a. The bottleneck is the worker with the highest processing time (across activities), which is Worker 2 (60 seconds) b. Capacity of the line is decided by the processing time of the bottleneck step. Hence we have Capacity = 1/ 60 sec = 60 units/hour c. Utilization is given by Flow Rate/ Capacity. Hence, we have Utilization = 45 sec/ 60 sec = 75%. d. As we are facing an empty system, the first unit would take (50+60+30+45+40)=225 seconds to go through the system. Hence, Flow time = 225 + (100 - 1)*60 = 102.75 minutes e. Labor Utilization is given by Labor Content / ( Labor Content + Idle Time). Total Labor Content can be calculated as (50+60+30+45+40)=225 seconds. Idle time for ea ch worker can be calculated as processing t ime of b ottleneck - processing time of worker . Hence, we have Labor Utilization = 225/ (225+10+30+15+20) = 75%. f. Direct Labor Cost = Labor Cost per Hour / Flow Rate = 5*$15/60 = $1.25/unit g. Again, there are multiple configurations that minimize completion time, but in all of these the processing time of the bottleneck resource is 55 seconds. Hence maximum achievable capacity is 1/ 55 sec = 65.5 units/hour. h. Direct Labor Cost = (30+20+35+25+30+45+40) sec * $15/hour = $0.9375/unit i. The bottleneck is worker 3, and process capacity is given by 1/ 75 sec = 48 units/hour Q4.8. Glove Design a. Cutting has a process capacity of 1 glove/2 minutes*60 minutes = 30 gloves/hour. Dyeing has a process capacity of 1 glove/4 minutes*60 minutes = 15 gloves/hour. Stitching has a process capacity of 1 glove/3 minutes*60 minutes = 20 gloves/hour. Packaging has a process capacity of 1 glove/5 minutes*60 minutes = 12 gloves/hour. Therefore, the capacity is a. 12 gloves/hour. b. The first statement is incorrect because packaging is the bottleneck. The second statement is incorrect because in a machine - paced line or conveyor belt, the unit spends the same amount of time at each station as the bottleneck. The fourth statement is incorrect because cutting is not the bottleneck. c. By reducing packaging time the process capacity increases is correct because packaging is the bottleneck.
Page 15 Read page 15 as text
Last revised May 2018 4 - 6 c. If the demand is 10 gloves/hour, then the implied utilization at packaging = 10/12 = d. 83.3%. d. A glove spends 5 minutes in each of 4 stations, so the flow time = 5*4 = c. 20 minutes . Q4.9. Worker Paced a. We know that Step 4 is the bottleneck and has a process capacity = to the capacity of the entire process because the utilization = 100%. We are given the fact that the process capacity = 36 units/hour, and Step 5 has a utilization of 40%. Therefore, the capacity of Step 5 = 36/0.4 = d. 90 units per hour. b. The step with the highest utilization is the bottleneck, or d. Step 4. c. The step with the highest utilization has the highest process capacity. Step 1 has a process capacity of 36/(4/30) = 270 units/hour. Step 2 has a process capacity of 36/(4/15) = 135 units/hour. Step 3 has a process capacity of 36/(4/5) = 45 units/hour. Step 4 has a process capacity of 36 units/hour. Step 5 has a process capacity of 36/(2/5) = 90 units/hour. Therefore, the step with the highest capacity is a. Step 1. d. There are 5 workers per hour to make 36 units. The wages per hour, then = 5*$36 =$180 in labor costs to make 36 units. Therefore, the direct cost of labor per unit = $180/36 = a. $5 per unit.
Page 16 Read page 16 as text
Last revised May 2018 5 - 1 Matching Supply with Demand: An Introduction to Operations Management 4e Solutions to Chapter Problems Chapter 5 Batching and Other Flow Interruptions : Setup Times and the Economic Order Quantity Model Q 5 .1 Window Boxes a) The production cycle consists of setup to produce part A (120 minutes), produce A (1 minute per part), setup to produce B (120 minutes), and produce B (1 minute for two sides). The total setup time in this production cycle is 240 minutes. The processing time for the two components is 2 minutes. There are 360 component sets produced in each production cycle. So the capacity of the stamping machine is 360 / (240 + 2 x 360) = 0.375 units per minute. b) We want to choose a batch size so that the capacity of the stamping process is the same as the capacity of the assembly process. The capacity of the assembly process is (1/27 units per minute) x 12 workers = 12/27 units per minute. The desired batch size is found using the following equation: batch size = (flow rate x setup time) (1 - flow rate x processing time). Hence, batch size = (12/27 x 240)/(1 - 12/27 x 2) = 960. c) The batch size is 1260 part A. Because this batch is larger than 960 (from question 5.1b), the bottleneck is assembly. Hence, the flow rate of part A is 12/27 part units per minute (the capacity of assembly). The processing time of part A is 1 min. Average inventory = ½ x 1260 units x (1 – 12/27 units per minute x 1 minute per part) = 350 part As. Q 5 . 2 Two - step a) Capacity of step B is 5 / (9 + 0.1 x 5) = 0.53 units per minute. The first activity makes 1 unit per minute, so the bottleneck is the second step. b) The flow rate is determined by the bottleneck, which is step A, and equals 1 unit per minute. The processing time at step B is 0.1 min per unit. The average inventory with a batch size of 15 is ½ x 15 x (1 - 1 unit per min x 0.1 min per unit) = 6.75 units. c) The desired flow rate is 1 unit per minute because that is the capacity of step A. Recommended batch s ize = 1 x 9 / (1 - 1 x 0.1) = 10 Q 5 . 3 Simple Set - Up a) First, we calculate the process capacity at each step using the formula for process capacity with batching: B / S + T b where B = batch size, S = set - up time, and T b = time to process the entire batch. So, the first step has a process capacity of 50 units / (20
Page 17 Read page 17 as text
Last revised May 2018 5 - 2 minutes + (1*50) minutes) = .714 units/minute = 42.86 units/hour. The second step has a process capacity of 50 units / (2*50) minutes = 30 units/hour. The third step has a process capacity of 50 units / (1.5*50) minutes = 40 units/hour. Therefore, the process capacity of the entire process = 30 units/hour . b) The only step that is dependent on the batch size is Step 1. With a batch size of 10 units, the process capacity of the first step becomes 10 units / (20 minutes + (1*10) minutes) = 10 units / 30 minutes = 20 units/hour. Therefore , Step 1 becomes the bottleneck. c) In order to determine an optimal batch size, we set the process capacity of Step 1 (the only step dependent on batch size) equal to the process capacity of the bottleneck capacity. The bottleneck capacity is 30 units/hour, or 1 unit every 2 minutes. So, we solve for B using the following formula: 1 unit / 2 minutes = B / (20 minutes + B minutes) B = 20 units . If B < 20 units, then Step 1 becomes the bottleneck and the capacity of the entire process decreases. d) Based on the answer to part (c), with a batch size of 40 the bottleneck is step 2 and the Flow rate is 30 units/hour. The processing time at step 1 is 1 min/unit, which converted to hours is 1/60 hour/unit. Average inventory after step 1 is therefore = ½ x 40 units x (1 - 30 units/hour x 1/60 hour / unit) = 10 units. Q 5 . 4 Set - Up Everywhere a) Capacity = B / ( S + B x Processing Time) = 35 parts / (30 minutes + ( 35 x 0.25) minutes) = .903 units/minute = 54.19 units/hour b) Step 2 is never the bottleneck because its processing time and setup time are always less than Step 1’s processing time and setup time. So the task can be simplified to determining for what values Steps 1 and 3 are the bottleneck. The processing time for the two steps are equal when 30+0.25B = 45+0.15B, or when B=150. For batches smaller than 150 parts, Step 3 is the bottleneck. For batches larger than 150 parts, Step 1 is the bottleneck. Q 5 . 5 JCL a) Capacity of a step is given by B atch Size/ (Set - Up - Time + Batch x Processing Time). Using this formula, the capacity of the three steps can be calculated as: Deposition: 100/ (45+0.15*100) = 1.67 units/min = 100 units/hour Patterning: 100/ (30+0.25*100) = 1.82 units/min = 109 units/hour
Page 18 Read page 18 as text
Last revised May 2018 5 - 3 Etching: 100/ (20+0.2*100) = 2.5 units/min = 150 units/hour T he bottleneck is the “deposition” step and it determines process capacity. b) If batch size is B, then processing time of step 3 is 20 + 0.20B which is always le sser than the processing time of step 2, 30 + 0.25B, for a positive value of B. Hence step 3 can never be the bottleneck. c) Under the new technology, the process capacity of step 1 is no longer dependent on batch size and is (1/ 0.45 min/unit) = 2.22 units/min. This is clearly the maximum overall process capacity that can be targeted. Since the capacity of step 2 can never exceed the capacity of step 3 (since step 2’s run time and setup time are both higher), we set the batch size so the capacity of step 2 matches 2.22 units/min. Thus, t he target batch size = Target capacity x Setup time / (1 – (Target capacity x Processing time)) = 2.22 units/min x 30 min / (1 – (2.22 units/min x 0.25 min/unit)) = 150 units . Q 5. 6 Kinga Doll a) The process capacity of molding = 500 / (15+(.25*500)) = 3.57 dolls/minute = 214.9 dolls/hour. The process capacity of painting = 500 / (30+(.15*500)) = 4.76 dolls/minute = 285.7 dolls/hour. The process capacity of dressing = 1/.3 = 3.33 dolls/minute = 200 dolls/hour. Therefore, the process capacity = 200 dolls/hour. b) For molding the target batch size = Target capacity x Setup time / (1 – (Target capacity x Processing time)) = 3.33 dolls /min x 15 min / (1 – ( 3.33 dolls /min x 0.25 min/ doll )) = 300 dolls For painting the target batch size = Target capacity x Setup time / (1 – (Target capacity x Processing time)) = 3.33 dolls /min x 30 min / (1 – ( 3.33 dolls /min x 0. 1 5 min/ doll )) = 200 dolls Therefore, the optimal batch size = 300 units. (If the smaller batch size were selected, then molding’s capacity would be too low.) c) The flow rate is the minimum of the process capacity, which is 3.33 dolls/minute or 200 dolls/hour, and demand. We know demand = 4000 dolls/week, with a 40 - hour work week. Therefore, the demand = 100 dolls/hour, which is less than the process capacity. Therefore, the current flow rate = 100 dolls/hour or 1.67 dolls/minute. For molding the target batch size = Target capacity x Setup time / (1 – (Target capacity x Processing time)) = 1.67 dolls /min x 15 min / (1 – ( 1.67 dolls /min x 0.25 min/ doll )) = 42.9 dolls
Page 19 Read page 19 as text
Last revised May 2018 5 - 4 For painting the target batch size = Target capacity x Setup time / (1 – (Target capacity x Processing time)) = 1.67 dolls /min x 30 min / (1 – ( 1.67 dolls /min x 0. 1 5 min/ doll )) = 66.7 dolls Again, choose the larger batch size so that the flow rate isn’t decreased 0 - t he optimal batch size is 6 6.7 . Q5. 7 PTest a) PTest can test 300 samples in 12*300/60+30 = 90min = 1.5hour. The capacity is 300 samples/1.5hours = 200 samples/hour. b) The smallest batch size that achieves a flow rate of 2.5 samples per minute is 2.5 * 30/(1 - 12/60*2.5) = 150 samples. c) The number of basic tests per minute = 70 / (15/60 * 70 + 1.5*30+20) = 70/82.5 = 0.848 Q5 . 8 Gelato a) Each batch consists of a set of three flavors. The total setup time is ¾ + ½ + 1/6 = 17/12 hours. The desired flow rate is 10 + 15 + 5 = 30 kgs/hr. The processing time is 1/50 hrs/kg. The desired batch size for the set of three is 30 x 17/12 / (1 - 30 x 1/50) = 106 kgs. b) Fragola is 10/30ths of demand, so produce (10/30) x 106 = 35.33 kgs of fragola c) Chocolato is 15/30ths of demand, so the chocolato batch is (15 / 30) x 106 = 53 kgs. The flow rate of chocolato is 15kgs/hour. The Processing time for chocolato is 1/50 hr/kg. So average inventory = ½ x Batch size (1 - Flow rate x Processing time) = ½ x 53 x (1 - 15 x 1/50) = 18.55. Q5.9 Carpet a) The flow unit is a yard of carpet. T otal demand = 100+80+70+50=300yrds/hr . S etup time = 4 carpets x 3 hr per carpet = 12hr . Processiong time=1hr/(350yrds/hr) = 0.002857hr . Target batch size = =12hr*300yrds/hr/(1 - 300yrds/hr*0.002857hr)=25200yrds . Of the carpet produced per production cycle, 100/300 th of it is carpet A. Hence, b atch size of carpet A = 25 , 200*100/300=8400 b) Batch size for carpet A is 16,800. Flow rate for carpet A is 100 yards/hr and the Processing time is 1/350 hr /yard. Thus, Average inventory = ½ x Batch size (1 - Flow rate x Processing time) = ½ x 16,800 x (1 - 100 x 1/ 350 ) = 6,000 yards. Q 5. 10 Catfood a) Holding costs are $0.50 * 15% / 50 = 0.0015 per can per week. Note, each can is purchased for $0.50, so that is the value tied up in inventory and therefore determines the holding cost. The EOQ is then 2160 0015 . 0 500 * 7 * 2 = T. b) he ordering cost is $7 per order. The number of orders per year is 500/EOQ. Thus, order cost= 62 . 1 500 * 7 = EOQ $/week=81$/year .
Page 20 Read page 20 as text
Last revised May 2018 5 - 5 c) The average inventory level is EOQ/2. Inventory costs per week are thus 0.5*EOQ*0.0015 = $1.62. Given 50 weeks per year, the inventory cost per year is $81 . d) Inventory turns=Flow rate / Inventory Flow Rate= 500 cans per week Inventory=0.5 * EOQ Thus, Inventory Turns= R / (0.5*EOQ) = 0.462 turns per week = 23.14 turns per year . Q 5.1 1 Beer Distributor The holding costs are 25% per year=0.5% per week=8*0.005=$0.04 per week a) EOQ= 6 . 223 04 . 0 10 * 100 * 2 = b) Inventory turns = Flow Rate / Inventory = 100 x 50 / (0.5 x EOQ) = 5000 / EOQ = 44.7 turns per year . c) Per unit inventory cost = unit / $ 089 . 0 100 10 * 04 . 0 * 2 = d) You would never order more than Q=600 For Q=600, we would get the following costs: 0.5*600*0.04*0.95 + 10*100 / 600 = 13.1 The cost per unit would be 13.1/100=$0.131 The quantity discount would save us 5%, which is $0.40 per case. However, our operating costs increase by $0.131 - 0.089 = $0.042. Hence, the savings outweigh the cost increase and it is better to order 600 units at a time. Q 5 .1 2 Millenium Liquors The f ixed cost of refrigeration can be ignored because that cost does not change as we vary our order quantity. a) W eekly holding cost 15%/50 per week * 120 $/case = 0.36 $/week . b) The ordering cost is $290+$10 = $300. EOQ= 9 . 273 36 . 0 45 * 300 * 2 = cases per orde r. c) We would get slightly lower ordering costs, which results in more frequent orders and lower inventory Q 5 .1 3 Powered by Koffee The holding costs are $1.50 per month ($1 storage and $0.50 capital) a) E OQ= 27 . 75 5 . 1 50 * 85 * 2 =
Page 21 Read page 21 as text
Last revised May 2018 5 - 6 b) Order frequency: (12 * 50) / EOQ = 8 times per year c) Average inventory is EOQ/2. So m onths of supply = (EOQ / 2) / 50 = 0.75 months d) inventory costs per month = ( EOQ / 2 ) * 1.50 = 56.46 $ / month e) The monthly holding cost per bag is $1 + 0.02 x 2 0 = 1.4 . Annual purchase quantity is 12 x 50 = 600 bags. The average inventory will be 600 / 2 = 300, and so the mon thly holding cost is 300 x $1.4 = $4 20 . The yearly holding cost is 12 x $4 20 = $5 040 . The annual purchase cost is 600 x $20 = $12,000. The total annual cost of this option is $ 12,000 + $500 + $5 040 = $1 7,540 . The current system operates at costs of 12* 5 . 1 * 50 * 85 * 2 +600 x 25=16,355 Thus, the original system is cheaper .
Page 22 Read page 22 as text
Last revised May 2018 6 - 1 Matching Supply with Demand: An Introduction to Operations Management 4e Solutions to Chapter Problems Chapter 6 The Link between Operations and Finance Q 6 .1. Crazy Cab a) see tree below b) see tree below c) Value drivers include the % of distance driven empty, the number of trips per day, and the distance of the trip. This is a high fix cost business with lots of capital, thus the more revenue you can squeeze out of the cabs, the more money you make. And interesting issue would be to see if by reducing the time the cab drives empty, one could increase the number of trips further d) Similar to the airline ratios discussed previously. We can look at labor efficiency as: Revenue/ labor cost = Revenue / mile * miles/trip * trips / day * days/ labor cost The first ratio is the pricing power, the second the length of a trip, the third how many trips we get out of a cab, and the fourth is a measure of wage rates.
Page 23 Read page 23 as text
Last revised May 2018 6 - 2 Return on Invested Capital 46 % Margin $644 k Invested Capital $1.4M Revenue $2.336M Cost $1.4M (labor) +$292 k (fuel) Working capital Fixed capital Trips per cab: 40 trips/day*365days/year # of cabs: 20 Price per trip # of trips Price per mile: $2 Fixed fee: $2 Distance: 3 miles Fuel & Mntnce cost Labor Cost: 20 drivers * 24hours/day * 8$/hour.driver*365days/year Number of cabs: 20 Capital per cab No information given in question; relatively small Cab: $20k Medaillon : $50K Distance : 20 cabs*40 trips/day.cab*3 miles/trip* * 365days/year*(100/60) $0.20 per mile # of drivers: 20 Hourly wage: $8
53 more pages in the full document
Unlock it once and it stays in your library, ready to chat with or turn into flashcards.
Unlock the full documentMore Operations Management study materials
See all Class Notes
Matching Supply with Demand: An Introduction to Operations Management 3rd Edition Class Notes
Operations Management
13 pagesMay 2025 Textbook Guides
Solution Manual for Operations and Supply Chain Management, 14th Edition
Operations Management
342 pages133downloadsFeb 2025 Textbook Guides
Managing Quality: Integrating the Supply Chain, 6th Edition Solution Manual
Operations Management
262 pages115downloadsFeb 2025 Textbook Guides
Operations Management, (Mcgraw-hill Education Operations and Decision Sciences) 1st Edition Solution Manual
Operations Management
153 pages91downloadsFeb 2025 Textbook Guides
Solution Manual for Introduction to Materials Management, 8th Edition
Operations Management
44 pagesMay 2025 Exam Guides
Operations Management, 5th Canadian Edition Test Bank
Operations Management
1208 pagesMay 2025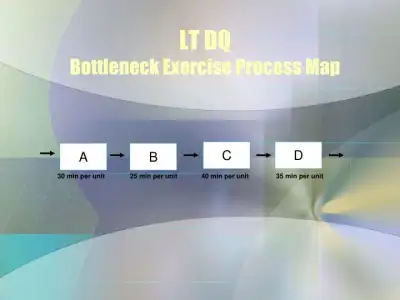 Class Notes
LT DQ Bottleneck Exercise Process Map
Operations Management
1 pageMay 2025 Class Notes
Lecture Notes for Operations Management, 2nd Edition
Operations Management
95 pagesMay 2025
Study this document with CramX
Once it is in your library, every tool can work from it.