

Revision Notes for Introduction to Materials Management, 8th Edition
- Operations Management
- 44 pages
- Shared May 2025
Revision Notes for Introduction to Materials Management, 8th Edition offers comprehensive revision notes designed to highlight key points from your class discussions.
Preview 14 of 44 pages
See the first 14 pages exactly as they appear in the document.
Page 1 Read page 1 as text
1 Stephen N. Chapman J. R. Arnold Ann K. Gatewood Lloyd M. Clive Case s tudy t ea C hing n otes for i ntrodu C tion to Materials Manage M ent, 8e Z03_CHAP6323_08_SE_CASE_WEB.indd 1 12/1/15 4:00 PM
Page 2 Page 3 Read page 3 as text
2 Case study t able of Contents Fran’s Flowers–Chapter 1 439 Meridian Water Pumps–Chapter 2 441 Williams 3D Printers–Chapter 2 443 Acme Water Pumps–Chapter 3 444 MasterChip Electronic–Chapter 3 445 Macarry’s Bicycle Company–Chapter 3 446 Apix Polybob Company–Chapter 4 448 Benzie Products–Chapter 4 450 Wescott Products–Chapter 5 453 Johnston Products–Chapter 6 456 Crofts Printing–Chapter 6 458 Melrose Products–Chapter 6 459 Let’s Party!–Chapter 7 461 Connery Company–Chapter 7 462 Northcutt Bikes: The Forecasting Problem–Chapter 8 464 Hatcher Gear Company–Chapter 8 467 Randy Smith: Inventory Control Manager–Chapter 9 468 Carl’s Computers–Chapter 11 470 CostMart Warehouse–Chapter 12 473 Metal Specialties, Inc.–Chapter 13 475 Cheryl Franklin, Production Manager–Chapter 14 476 Murphy Manufacturing–Chapter 15 476 Accent Oak Furniture Company–Chapter 16 478 Z03_CHAP6323_08_SE_CASE_WEB.indd 2 12/1/15 4:00 PM
Page 4 Read page 4 as text
Teaching Notes for Introduction to Materials Management, 7e 3 f ran’s f lowers Chapter 1 Case Study Teaching Notes Fran’s Flowers is a good case to use early in a course of study, because it illustrates two important areas (service design and operations strategy) in a case format that is com- pletely qualitative, and therefore less threatening to some students as they make their first entrance into materials management. It can also be used to start students thinking about the quantitative aspects of materials management, both from a data gathering and data analysis aspect, as one of the direct case questions (#2) asks students to consider the data collection needs as well as how they would suggest using this data. This presents a good opportunity (usually at the conclusion of the primary analysis) to have an open, “brain- storming” discussion. This can be used not only to start student thinking about quantita- tive analysis, but can also be used as an “icebreaker” to allow students to feel comfortable about open class discussions. t he Problem Fran clearly stated that she intended to focus on the specialty make-to-order flower arrange- ments. Clearly, in such a business, the major operational focus should be on artistic capabil- ity, flexibility, design, and close communication with the customer. The volume would be fairly small, but the margin on each order would be fairly large. The order-winning aspects of such a business would clearly be availability, design, and flexibility. Once those characteristics have been developed, a discussion of the importance of location can be initiated. In the make-to-order business, location could be expected to be insignificant, as the case indicates when it discusses how Fran and Molly usually visit the clients to obtain the order, rather than the other way. In such a situation it really doesn’t matter where she locates as long as she has space to store the flowers and make the arrangements. Some student will immediately jump on the now-obvious mistake that Fran made. She selected a location in a highly visible strip mall. In such a location it should be ex- pected that people will walk in a flower shop with the idea of making spot purchases of flowers. In other words, she selected a location without considering the strategic impacts. It might have worked out without a problem if she would have just turned away the cus- tomers wanting the spot purchases, but the financial benefits of such an apparently easy sale was too appealing. As soon as Fran started accommodating those walk-in customers, she had evolved into two separate businesses with two separate operational strategy models. The walk-in busi- ness was, of course, a make-to-stock business with all the typical characteristics of such a business. The contrasts are summarized in the following table. Such a table can be easily developed during the class discussion to enable all students to clearly see the contrast in the service businesses: Make-to-order Make-to-stock Price Not Sensitive Sensitive—Order Winner Location Not Sensitive Critical Design Order Winner Standardized Skill Level Very High Fairly Low Volume Very Low Higher Variety of Design Each One Different More Standard Operational Focus Close Customer Contact Standardized, Low Cost Inventory Can Order as Needed High—Standard Arrangements Not only has she gotten herself into a dual business situation (of which she origi- nally had no interest in and has minimal managerial skills to run), but now customers in the make-to-stock business are trying to force her to move even more away from her Z03_CHAP6323_08_SE_CASE_WEB.indd 3 12/1/15 4:00 PM
Page 5 Read page 5 as text
4 Case study core. The consideration to have the shop open for a longer duration, open a second loca- tion, and become part of a national delivery service will pull her away from her central business focus even more. a pproaches There are really three basic approaches that appear to make sense, although some students will come up with logical variations on these three: Do nothing—This is always an alternative, and is frequently the least desirable one for a number of reasons. It would continue the problems outlined in the case and quite likely cause erosion of her business, as it appears she cannot give proper attention to either business under the current circumstances. Expand the make-to-stock business—Given that she apparently has a good loca- tion, this business could be attractive if run effectively. Fran, however, does not con- sider the business as the one most attractive to her. She just prefers to use her design talents on the make-to-order. One method to allow for effective expansion is to hire a full-time, experienced person to completely take over the make-to-stock business. This person could be evaluated on a profit basis, but be given almost free reign to expand the business in any direction that will prove profitable. Fran could then concentrate her efforts on the make-to-stock, and it is highly likely that both businesses would become successful, allowing for at least some synergistic effects as customers for one business would, under the right circumstances, buy from Fran if they had a need for flowers for another purpose. Eliminate the make-to-stock business—One potential problem with the expansion of the make-to-stock business is the requirement for a large amount of capital (this, in fact, should be one of the data items students should mention for case question #2). Eliminating this business would allow her to concentrate on her core business, with less need for capital. The largest problem with this is the potential loss of profitability with the make-to-stock business, and she still has the location issue. If she wants to maintain the present location, she should take steps to clearly identify the nature of the business to possible walk-in customers. Given that the strip mall is popular, however, the lease costs may be higher than that she would have to pay given that location is not very important to the make-to-order business. She might be better off financially to seek a location with a lower cost. Location, again, is not critical in the make-to-order business. Conclusion Another opportunity for discussion is presented as students debate these options, or may, in fact, create others. This discussion can be again used to bring in the data questions. You may wish to ask the students the criteria they should use to make the final decision. Much of these criteria will probably be dependent on gathering certain information. You may or may not wish to spend much time on the implementation question. Such a discussion tends to be less interesting to students and more “mechanical” in nature, but if you wish to use the case to have students think about the detailed design issues for a service business, you may want to spend some time with it. This case was based on a real situation in a real flower shop. You may wish to inform the students that the real “Fran” decided to use her skills and desires to concentrate on the make-to-order business, but the potential for the walk-in business was too attractive to eliminate, especially given her location. She hired an experienced retail manager to man- age the walk-in business as a profit center. The manager was given permission to manage that business in any fashion he or she wished, but part of his or her compensation was based on profit sharing, giving the manager plenty of incentive to make the store profit- able. Fran and Molly worked in the back room, but could serve as advisors to the walk-in business as requested by the new manager. Fran and the new manager would meet on a regular basis to discuss the overall business and look at flower needs, constantly try- ing to evaluate the possibility of different approaches to combine needs for flowers and minimize the overall cost of purchasing stock. As of the writing of this case the approach appeared to be working. Z03_CHAP6323_08_SE_CASE_WEB.indd 4 12/1/15 4:00 PM
Page 6 Read page 6 as text
Teaching Notes for Introduction to Materials Management, 7e 5 Meridian w ater Pu MP s Chapter 2 Case Study Teaching Notes This case is a fairly simple case to work on analytically, yet can provide the basis for a good discussion about the trade-offs involved with making a good production plan or Sales and operations plan. While there are clearly differences in the financial results of the possible plans, there are clearly nonfinancial issues that can and should be discussed in order to give students a better overall perspective involved with this important planning process. Here are sample solutions to the assignment questions: 1. Developing a level production plan is fairly easy. The total demand for the six months is 4650 units. Since the current inventory is 50 and the target inventory for the end of the six month is 25, we reduce the required production for the six months to 4625 (4650–25). Dividing the 4625 by the six months, we would be required to make 771 pumps per month. Dividing the 771 by 25 (the number of pumps one worker can make in one month), we would need 30.8 workers. Rounding that to 31 workers, we have the following result: ■ ■ We need to hire 11 workers (there are currently 20, and we need 31) ■ ■ There is an upfront cost of $1100 ($100 hiring cost for each worker) ■ ■ The monthly production will be 775 (31 workers × 25 pumps per worker) ■ ■ The inventory at the end of month 1 will be 225 (production of 775 plus existing inventory of 50 = 825, then subtract the production of 600) Month 1 2 3 4 5 6 Demand 600 750 1000 850 750 700 Production 775 775 775 775 775 775 Inventory 225 250 25 –50 –25 50 Inventory cost $1125 $1250 $125 $0 $0 $250 The total inventory cost is $2750 The total hiring cost is $1100 The total extra cost of the level plan is $2750 + $1100 = $3850 There are several qualitative issues that can and should be discussed here. Three of the more important ones may be as follows: ■ ■ There are two months when shortages appear. There is no indication how custom- ers will react. For example, if the customers are willing to wait for one to two months, then certainly there will at least be some loss of goodwill. There is a high probability that customers would not be willing to wait if they could obtain the product from a competitor (given that water pumps are a common product, this is highly likely). In that case a real financial cost is the loss of profit from those lost sales, and potentially some permanent loss of those dis appointed customers. At a minimum, there is likely to be some cost in filling the backorders. ■ ■ As indicated in the case, such shortages also require sales people to make addi- tional visits to customers to calm their anger. Such visits might cost some real dollars and also create some anger and discouragement within the sales staff. ■ ■ There is an assumption that the newly hired 11 people will be able to produce a full production (25 pumps per month) immediately. Most production jobs entail a learning curve, implying that the production of 775 total pumps in month 1 may be overly optimistic. 2. The chase plan is also fairly easy to develop. To create it, the assumption is made that the target inventory of 25 can be accomplished in the first month. To obtain the num- ber of people needed each month, the demand for that month is divided by 25 (the number of pumps one worker can make in one month). The only exception is the first month, when we assume that 25 units of demand can be taken from inventory to get to the target level immediately. Z03_CHAP6323_08_SE_CASE_WEB.indd 5 12/1/15 4:00 PM
Page 7 Read page 7 as text
6 Case study Month 1 2 3 4 5 6 Demand 600 750 1000 850 750 700 People Needed 23 30 40 34 30 28 People +/– 3 7 10 –6 –4 –2 Inventory 25 25 25 25 25 25 Hire/Layoff Cost $300 $700 $1000 $600 $400 $200 The total hire/layoff cost for the six months is $3200. The inventory cost for each month is 25($5) = $125. For the full six months the cost for inventory is $750. The total cost for the chase strategy, then, is $3950. That is only slightly higher than the level strategy ($100). As with the level strategy, however, there are qualitative issues that should be discussed. Included should be the following: ■ ■ From a customer perspective, this approach is clearly better than the level plan that represents at least two months of inventory shortages. One might argue (and in a real situation even calculate) that this approach is financially better, in that the potential cost of lost profitability was not included in the level schedule analysis. ■ ■ The largest qualitative cost in this chase plan is the constant movement of people in and out of production. This ignores several potential “hidden” costs, including the following: ■ ■ The learning curve impact of the new people. The analysis assumes that a new person can produce at the same rate as an experienced one. This is seldom the case. ■ ■ The issue of employee loyalty. The production people will likely get the impression (rightly so) that the company has little or no loyalty to the feelings and needs of the workers. In that case, it would be likely that the employees will also have little feeling of loyalty. That can impact not only morale, but also productivity improvement efforts. ■ ■ A little recognized issue is the impact of employee “guilt.” In some cases employees who escape a layoff will feel guilty. While often relieved that they kept their job, they will sometimes express the feeling of “why did I survive—I feel guilty that I have my job while some of my friends on the production line lost their jobs.” 3. The following represents a hybrid plan. It has a level schedule for the first three months (until the demand grows to the point where shortages would occur), then has a level schedule for the next two months, then starts to reduce employees as the lower demand part of the cycle again starts. Month 1 2 3 4 5 6 Demand 600 750 1000 850 750 700 People Needed 23 30 40 34 30 28 People +/– 12 0 0 –2 0 –1 Production 800 800 800 750 750 725 Inventory 250 300 100 0 0 25 Hire/Layoff Cost $1200 $0 $0 $200 $0 $100 Inventory Cost $1250 $1500 $500 $0 $0 $125 The total cost of this plan (inventory plus hire/layoff costs) is $4875. From this purely financial analysis of these two extra costs, this plan would not be preferable. If, however, all the qualitative costs discussed above (and their potential associated financial implications) are to be considered, this approach may be preferable and selected. Specifically, it has a reasonably small impact on layoffs and also prevents shortages that could impact customers. Z03_CHAP6323_08_SE_CASE_WEB.indd 6 12/1/15 4:00 PM
Page 8 Read page 8 as text
Teaching Notes for Introduction to Materials Management, 7e 7 4. There is only one hybrid approach presented. This question presents a great opportunity for students to present their own plans and discuss the pros and cons of each. A good discussion here can leave students with a much stronger perspective of the issues and advantages of developing good production plans. w illia M s 3 d Printers Chapter 2 Case Study Teaching Notes This case has an advantage in that it can be used for discussing the strategic issues often surrounding the development of longer term S&OP planning, where additional capacity is possibly needed. But if students are not at a level where that is appropriate, then the case can be more simply used as a discussion of some of the options available for a company in this situation to use, and some of the pros and cons of each. You may find that even for students not familiar with strategic thinking that some may move in that direction based on their experience and basic logic. The environment described and the issues facing the company are fairly common for a start-up organization in a rapidly growing market typical of the introduction phase of a prod- uct life cycle. You may wish to point out that often in such a market many small companies trying to enter the market is typical, but over time most will fail, either because of an inferior design, a lack of flexibility to understand the market, or the inability to find ways to grow in the market. As successful companies in the market grow, they are able to gain from the advantages of growth, including economies of scale. You may wish to point out that since the entire market is growing at this point, individual companies may experience growth without experiencing a lot of competitive pressure. This is because growth can occur without actually growing market share (assuming the company grows at the same rate at which the market grows). Later on in the life cycle when the market growth slows considerably, the competition between survivors will tend to increase as the only way they can obtain growth is through taking market share from another company. How much of a discussion of this you feel appropriate should be based on the background of the students. You can also refer them to the first few pages of Chapter 14 where the product life cycle is briefly discussed. The case can be discussed without this life cycle discussion, focusing primarily on the key issue of dealing with longer range sales and operations planning (S&OP) in this kind of environment. It certainly can bring out many of the trade-offs inherent with the devel- opment of any S&OP process that almost any company has to go through, although in this case inventory does not seem to be a major problem (again somewhat typical in what ap- pears to be a make-to-order environment). The key trade-offs here appear to lie within the concepts of how to best manage rapidly growing sales forecasts. Specifically, they need to plan for longer range resources and how to pay for them. Certainly, one alternative is for them to maintain their current size and only take or- ders that they can produce within their existing facility and staffing. Some students may wish to take that option, and could justify it by stating that it would allow the facility to only take orders with the highest possible profit margin. Given that the design for each order is apparently not standard, the price is likely not standard either. If they do negotiate price, it gives them the option of taking or not taking a particular order. Some compa- nies in this type of market will elect to take this approach, and it can work as the market matures if the company can successfully identify and defend a specific niche where they can provide good products and services. It is not clear that this would be the preferred ap- proach here, and certainly it would appear that the sales and marketing manager, at least, would need to be convinced. Also, if they stay small as the market matures, they may face other problems—the design of a product tends to become more standard as the market ma- tures, and also price becomes more sensitive. This type of discussion may be too advanced for your students, but asking them to consider what has happened in recent years to the product with which they may be familiar with may help—consider “smart” televisions, cell phones, and almost any other electronic device. If the growth option is taken, then Pamela’s concerns need to be addressed. The deci- sion to grow the business needs to include a good plan as to how. As Pamela points out, Z03_CHAP6323_08_SE_CASE_WEB.indd 7 12/1/15 4:00 PM
Page 9 Read page 9 as text
8 Case study growth in the production area may need to appear something like a “step function,” where large “chunks” of production capacity are added. Smoothing out added production capac- ity would seem to be difficult here, although it should be pointed out (and some students may suggest) that sometimes smoothed addition of capacity can be obtained by subcon- tracting the work. If the discussion goes in this direction, student should be aware that in those cases, it is more difficult for the company to control the work, especially in terms of quality, but also cost and delivery. Still this may be a very attractive alternative for some students. If they decide to grow internally with the “chunks” of capacity, they need to address that likely at first they would have an excess of capacity since the sales are less likely to grow in matching “chunks” of orders. Options possibly exist, however. One would be to offer other companies some of the added capacity for short-term subcontracting work. Another would be to build some inventory of more standard parts of the printers. The inventory option would mean even more added cost up front, but could allow them to postpone the next needed “chunk” of capacity assuming the market continues to grow. If the students are at a level where discussion of this option evolves some strategic points, you may wish to point out that addition of capacity in this early life cycle market often should lead the growth of demand. While that option tends to cost more in the short term, products in this type of market tend to be much more sensitive to delivery than they are to price, and the excess capacity (especially in a product with lots of design options) can help make delivery reliable, and they also tend to provide good margins (not being particularly price sensitive). On the other hand, facilities producing products in a more mature market tend to allow the addition of capacity to lag demand growth, preferring to use techniques such as working overtime and subcontracting as much as possible before turning to acquiring more capacity. The main point against adding a “chunk” of capacity is cost and the impact on profitability. Certainly, the concerns of the financial manager need to be considered, and it would be an important decision if the company wishes to forgo a profitability position for some time in the future to pay for the added capacity. Some students may point out that this may make them much more profitable in the future as they can serve more of the market. While that can be true, you need to point out that if growth continues, the company is likely to face a similar issue about adding even more capacity sometime in the future. Students should be made aware that these kinds of deci- sions must be made considering the overall strategy of the firm. They should be able to understand that even if you elect to forgo any detailed discussion around the life cycle and its characteristics. aCM e w ater Pu MP s Chapter 3 Case Study Teaching Notes The following is a master schedule using the case data. It is important to note that the projected balance ignores the forecast data for the first three weeks (because the demand time fence is 3 weeks), and from that point on the balance is computed from the larger of customer orders or forecast. Period 1 2 3 4 5 6 7 8 9 10 11 12 Forecast 90 120 110 80 85 95 100 110 90 90 100 110 Cust. orders 105 97 93 72 98 72 53 21 17 6 2 5 Proj. Balance (25) 220 123 30 250 152 57 257 147 57 267 167 57 MPS 300 300 300 300 ATP 30 58 209 287 The order request for week 5 of 45 units should be no problem, as the ATP of 58 for week 4 covers it nicely. At this point it might be helpful to teach students about ATP by challenging them with additional questions about future orders. For example, Z03_CHAP6323_08_SE_CASE_WEB.indd 8 12/1/15 4:00 PM
Page 10 Read page 10 as text
Teaching Notes for Introduction to Materials Management, 7e 9 What if the new customer order is for 70 in week 5? Still no problem. You could promise the 58 produced in week 4 and the additional 12 from the 30 ATP in week 1. Key point here—it is not important for the customer to know when the item is produced, only when they get it (an exception is an item with a short shelf life). What if the new customer order is for 100 in week 5? Now the issue is more complex. You could promise 88 (58 in week 4, 30 from week 1). For the rest of the request, there are three options: 1. You could ask the customer if you could give them 88 in week 5 and the rest in week 7. 2. If that option does not work for them, you could work with sales to ask if the other customer orders could accept some of their pumps at a later time, so you could split the shipment of their orders. 3. If that does not work, you need to check if you have the material and capacity to increase production by 12 units sometime during the next 5 weeks. If none of those options work, the only alternative is to tell the customer that you can deliver only 88 for them in week 5. t he MasterChi P e le C troni C s Co MP any Chapter 3 Case Study Teaching Notes Sally is confronted with a relatively common environment. Her product line is competi- tive, somewhat delivery time sensitive, variable in demand patterns (volume and timing), option-oriented, and made with components that have fairly short life cycles. The union contract is certainly a constraint, but she should be able to manage around it more ef- fectively. The measurement system focused on efficiency and utilization is also clearly a problem. This customer environment is one with variable orders in terms of size and options, and clearly the customers are sensitive to delivery reliability, especially when planned for something like a planned promotion. One could make the argument that at least part of the solution would be to “educate” the customers to provide more of their own planning information to MasterChip. That could very well help Sally’s own plan- ning, but that should be viewed as a long-term approach at best. Essentially, this envi- ronment sounds like at least an assemble-to-order (ATO) environment, a quite possibly a make-to-order environment for at least some of the products, and should be managed accordingly. First, it appears that Sally is relying on mostly short-term capacity planning (really reaction rather than planning) by using weekly layoffs and callbacks. The problems that appear in this environment are clear—excess capacity in parts of the facility and capacity shortages with lots of late orders in another part of the facility. Given that the demand patterns are somewhat erratic, you could assume that these capacity shortages and ex- cesses have a tendency to move from area to area over time. She could avoid a lot of this if she had more flexible workers (where she could move them from one area to another), but this would require a change in the union contract and also a comprehensive training program to give workers more transferable skills. She also would be helped if she could change worker hours with more flexibility than weekly. That, too, could be an issue for their next union contract negotiation. This implies that it may be very difficult to do and certainly will not help in the short term. Additionally, one could argue that the issues she faces with short-term capacity is really symptomatic of other parts of the planning system. The major problem here is that the company does not appear to do any effective longer range planning, as would be accomplished with a well-run sales and operations planning (S&OP) process and a well-managed master scheduling program. As it appears now, the sales force seems to take any order they can get with little regard for how well that order fits into a managerial agreed to long-range S&OP. Students should be made to realize that with an effective S&OP, where the timing, cost, and quantity of resources are taken into account, the “target” sales for a period may not represent the unconstrained forecast demand for sales, but instead be representative of the sales the company should obtain to best maximize Z03_CHAP6323_08_SE_CASE_WEB.indd 9 12/1/15 4:00 PM
Page 11 Read page 11 as text
10 Case study profits. Taking any order that comes along and blindly quoting a standard lead time clearly should not be done, especially in this type of volatile assemble-to-order environment. Because of the ATO environment, the master schedules should likely be developed at the option level. This will allow two very important activities to be done for the com- pany. First, the overall capacity can be managed at the rough-cut level to fit within the constraints established in the S&OP. Second, the master schedule can be established with available-to-promise (ATP) logic. It can be very powerful in this environment, especially if the sales force is trained what to look for in the ATP logic. A quick look, for example, in the situation described in the case, should have told the sales manager that he could prom- ise at most 200 of the A77 units in the standard lead time, but also could tell him when the rest of the order could be shipped—and this could be done without having to check with anyone from production. The final assembly schedule would be developed from the actual customer order based on the options selected, but if the S&OP is managed effectively and a rough-cut capacity plan developed from the master scheduling activity, then the chance of any major mismatch in capacity should be minimized. This case can be used for three different types of student groups. If the students are still at a fairly basic level in their understanding of planning systems, it can easily be used just to emphasize the value of S&OP and ATP logic, as well as the need for longer-range capacity planning and how this is done in S&OP and master scheduling. If the case is to be used with more advanced students, it could serve as an effective “launch” into discussion of two-level master planning, and “super planning” bills of material. Finally, the case can be used to initiate discussions about operations strategy (if ap- propriate for the level of students), using the understanding of the environment to influ- ence almost every aspect of the organization, including measurement systems (clearly a problem here) to planning systems, to priorities the organization should be putting on various aspects of union agreements if they exist, as they do in this case. Ma C arry’s b i C y C le Co MP any Chapter 3 Case Study Teaching Notes This case works well to allow students an opportunity to practice their skills on developing mas- ter schedules and also to practice using them to effectively promise orders. You may notice that without specifically stating so, this case is a typical approach using two-level master schedules with essentially a “super bill” approach that is often used in such an assemble-to-order environ- ment. In this case that approach was not specifically mentioned, but at the conclusion of the discussion in the case, you may wish to take the opportunity to introduce the generic concepts of super bills, two level master planning, and even option of overplanning to your students. You will likely note that while the planning time fence is defined as 20 weeks, there is no defined demand time fence and the master schedules are developed assuming demand time fence does not exists. Once the initial discussion of the questions in the case has been completed, you may wish to ask your students how, if at all, their solutions would change if a demand time fence is set. They will likely gain good insight on the use of the time fence if you set a couple of different time fences for discussion—say one time at 2 weeks and then at 5 weeks. If this option is taken, it may be instructive to have the students summarize the pros and cons of using demand time fences. The completed master schedules are as follows: Common parts (Frame, etc.). Existing inventory 40 Week 1 2 3 4 5 6 7 8 9 10 11 12 Forecast 50 55 60 62 65 65 68 70 75 75 80 85 Cust. Orders 56 52 45 33 70 50 35 60 20 20 0 0 Projected Inventory. 184 129 69 7 137 72 4 134 59 184 104 19 Master Prod. Sch. 200 200 200 200 ATP 54 45 120 180 Z03_CHAP6323_08_SE_CASE_WEB.indd 10 12/1/15 4:00 PM
Page 12 Read page 12 as text
Teaching Notes for Introduction to Materials Management, 7e 11 18-speed gear option Existing inventory 25 Week 1 2 3 4 5 6 7 8 9 10 11 12 Forecast 35 39 42 44 46 46 48 49 53 53 56 60 Cust. Orders 37 38 40 33 50 20 25 40 5 5 0 0 Projected Inventory. 138 99 57 13 113 67 19 120 67 14 108 48 Master Prod. Sch. 150 150 150 150 ATP 27 55 100 150 Straight handlebars Existing inventory 20 Week 1 2 3 4 5 6 7 8 9 10 11 12 Forecast 15 17 18 19 20 20 21 21 23 23 24 26 Cust. Orders 16 18 20 5 15 22 15 20 5 8 0 0 Projected Inven. 4 46 26 7 47 25 4 43 20 57 33 7 Master Prod. Sch. 60 60 60 60 ATP 4 17 8 35 52 Head and tail light set Existing inventory 5 Week 1 2 3 4 5 6 7 8 9 10 11 12 Forecast 10 11 12 13 13 13 14 14 15 15 16 17 Cust. Orders 2 12 10 8 15 9 7 11 2 1 0 0 Projected Inventory 25 13 1 18 5 22 8 24 9 24 8 21 Master Prod. Sch. 30 30 30 30 30 30 ATP 11 7 14 17 29 30 The solutions to the order inquiries: a. A customer is asking about an order of 32 of the bicycles for week 3. All 32 are to be 18-speed, 12 are to have straight handlebars, and 14 are to have the light set. While the order has no problem from the standpoint of the frame and common parts, only 27 of the 18-speed are available for week 3 and only 11 of the light set are available. There are enough handlebars for the order. The customer should be told that they can have 27 of their complete order for week 3 (the major con- straint is the 18-speed, where they are 5 short—they are only 3 short of the light set). The remaining 5 bicycles can be delivered for week 5, when the next MPS is scheduled for the 18-speed. The light sets will be available in week 4, but the last 5 of the order needs to wait for the 18-speed option. Of course, in this and in any similar situation the sales people always have the opportunity here to attempt to convince the customer to accept a different option in order to get their order complete in week 3. b. A customer is asking about an order of 60 of the bicycles for week 6. Fifty of them are to be 18-speed, 12 are to have straight handlebars, and 5 are to have the light set. There are plenty of frames and common parts (while only 45 are in ATP for week 5 and all can be used, the remaining 15 can be taken from the ATP in week 1). This situation is a good opportunity to emphasize to students that in the type of environment where items have long “shelf life,” the customer often doesn’t tend to care when the item is made—they are only concerned about when they can have it. The 18-speed option is also no problem, for the same reason. The same is true for the handlebars and light set. The customer should be told “sure, no problem.” Z03_CHAP6323_08_SE_CASE_WEB.indd 11 12/1/15 4:00 PM
Page 13 Read page 13 as text
12 Case study c. A customer is asking about an order of 20 of the bicycles for week 2. All are to be 18-speed, all are to have straight handlebars, and all are to have the light set. Again, there is no problem with the frames and common parts, the handlebars, and the 18 speed. The problem is the light set. Only 11 can be delivered with the light set in week 2, with 7 more delivered in week 4 and the last 2 in week 6. d. A customer is asking about an order of 110 of the bicycles in week 7. Sixty are to be 18-speed, 22 are to be straight handlebars, and 15 are to have the light set. There are only 99 frames and common parts available by week 7. The remaining will need to be promised in week 8. The 18-speed option is not a problem, the straight handlebars are not a problem, and the light sets are not a problem. The customer should be promised 99 in week 7 and the remaining 11 in week 8. At this point in the discussion you may find some students still confused. If that is the case, you may wish to create a few hypothetical orders of your own and have the students come up with solutions. Question 3 Suppose Macarry Bicycle managers discover that a major competitor has had to shut down its production for the next three months due to a major fire. The Macarry managers fully expect that many of the competitor’s customers will turn to Macarry Bicycles to fill their orders during this critical time. In fact, one of the competitor’s customers has already asked about an order of 250 of the models for delivery in week 5. What actions should Macarry take in this case? Be as specific as possible. Students need to realize that there are important reasons why planning time fences exist. They may be quick to realize that this situation represents an opportunity to get lots of unexpected orders, but to take those orders without the ability to deliver them threatens to alienate lot of potential new customers as well as existing ones. They will be tempted to add lots of MPS orders within the time fence. This presents the oppor- tunity to discuss why adherence to the planning time fences is so important. Point out that they might be able to evaluate component inventories and existing capacity and possibly squeeze a few more added to production, but by no means should they assume that because they can put a number in the master schedule that it will really happen. Certainly, they have more freedom outside the planning time fence, but the impact on component suppliers and internal production capacity still needs to be evaluated before adding lots of new production requirements immediately outside the planning time fence. You may also wish to initiate a strategic discussion—for example, with their existing ATP orders, should they take orders from one of these potential new custom- ers before they consider the needs of their regular customers? The danger is, of course, that as soon as the competitor recovers from the fire, its old customers may return to the competitor as a supplier. In the meantime, if Macarry Bicycles has alienated its regular customers by failing to be able to cover their regular orders, they may find that some of those regular customers may also leave them. aP ix Polybob Chapter 4 Case Study Teaching Notes Introduction This is a relatively basic case used to discuss the issues of managing dependent demand inventory, specifically using the concepts of MRP. The case starts with a discussion surrounding the problems using EOQ with reorder points. Not only is the reorder point inappropriate for dependent demand inventory in most cases, but they actually also seem proud that the inventory accuracy levels are “at least 80%.” Most people familiar with materials management will recognize that an 80% level is hardly acceptable for effective planning. Z03_CHAP6323_08_SE_CASE_WEB.indd 12 12/1/15 4:00 PM
Page 14 Read page 14 as text
Teaching Notes for Introduction to Materials Management, 7e 13 Most of the rest of the first part of the case deals with a description of some of the typical symptoms that one would expect when dealing with the kind of conditions devel- oped in the case. While these symptoms should not be the major focal point of the case, they should be discussed. Many students will gain insight by being challenged to explain why the symptoms described are likely to occur in such an environment. At this point the MRP calculations can be brought out. The MRP solution is presented at the end of this note. One of the first issues that should be mentioned is how the rela- tively “regular” production levels end up in quite “lumpy” demand for lower level compo- nents, brought on by lot sizing as the demand cascades down the bill of materials. In other cases, the ability of MRP to look ahead can show many other points that students can (or should) notice. For example, the scheduled receipt for item F is not needed in week 1, and can be de-expedited. Case d iscussion Questions The first two questions have been mentioned above. Others include the following: Question 3 MRP assumes an accurate database and also is (by itself) capacity insensitive. These issues should be pointed out to students (in case they fail to bring them out) as critical points that must be considered. In other words, the MRP solution will likely provide little benefit with only an 80% inventory accuracy, and will do little to prevent sales from over- promising orders unless the system is coupled with a good master schedule and capacity planning approach. Question 4 If there were only 250 of item E on hand instead of the 400 listed, the gross require- ment could not be met for week 2. This would cascade up to the final product (a good opportunity to discuss the concept of pegging). Where MRP could help is in at least two ways. First, it could point out the potential problem with enough time to poten- tially expedite the delivery of parts, thereby possibly preventing a problem condition. If, on the other hand, expediting is impossible, the nature of the shortage can be calcu- lated and customers notified with hopefully enough time to plan around the expected shortage. Question 5 One of the great values of MRP is the “look-ahead” capability, and this question addresses that capability. Often the phase-in of a new design will occur when the impact on existing inventory is at a minimum. A look at the MRP shows that perhaps the best time for the new design phase-in would be after week 10, when the inventory of the old part is very low. Some students may argue that the best time would be the order for week 2. That is not an incorrect conclusion, and gives the opportunity to discuss the pros and cons of phasing out small versus large amounts of old inventory designs. Question 6 This is a rather “open-ended” question that will allow students to be creative in their anal- ysis. Some items they may come up with are changes in the labor force, vacation planning, promotions, and planning for equipment maintenance. Question 7 While students may come up with actual numbers for this question (based on several assumptions), the primary purpose for the question is to generate thinking about the financial implications of the differences between the two approaches. What can clearly be shown is that for many of the items there would be serious shortages using the reorder point. In some cases (item E, for example), the reorder point would generate order before they are actually needed, increasing inventory holding costs. The part shortages will clearly produce expediting activity, and generate some of the symptoms discussed in the case as well. Z03_CHAP6323_08_SE_CASE_WEB.indd 13 12/1/15 4:00 PM
30 more pages in the full document
Unlock it once and it stays in your library, ready to chat with or turn into flashcards.
Unlock the full documentMore Operations Management study materials
See all Textbook Guides
Solution Manual for Introduction to Materials Management, 8th Edition
Operations Management
44 pagesMay 2025 Exam Guides
Introduction to Materials Management 8th Edition Test Bank
Operations Management
94 pagesMay 2025 Textbook Guides
Solution Manual for Operations and Supply Chain Management, 14th Edition
Operations Management
342 pages133downloadsFeb 2025 Textbook Guides
Managing Quality: Integrating the Supply Chain, 6th Edition Solution Manual
Operations Management
262 pages115downloadsFeb 2025 Textbook Guides
Operations Management, (Mcgraw-hill Education Operations and Decision Sciences) 1st Edition Solution Manual
Operations Management
153 pages91downloadsFeb 2025 Textbook Guides
Solution Manual For Matching Supply with Demand: An Introduction to Operations Management, 4th Edition
Operations Management
76 pages36downloadsFeb 2025 Exam Guides
Operations Management, 5th Canadian Edition Test Bank
Operations Management
1208 pagesMay 2025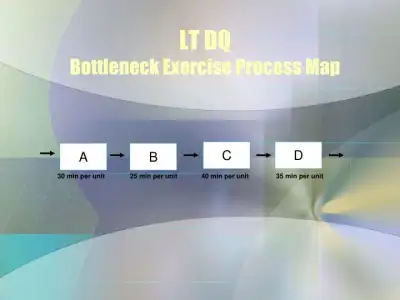 Class Notes
LT DQ Bottleneck Exercise Process Map
Operations Management
1 pageMay 2025
Study this document with CramX
Once it is in your library, every tool can work from it.